
Technical Drawings
DIN 357
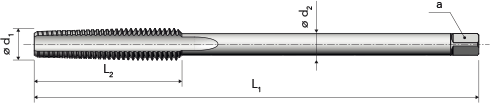
Articles
Scroll horizontally to view table data
| M | Ød1 | P | L1 | L2 | L3 | Ød2 | a | z |
 |
Article | |||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| [mm] | [mm] |
[mm] js 16 |
[mm] | [mm] |
[mm] h9 |
[mm] h12 |
[-] | [mm] | |||||
| M 4 | 4 | 0.7 | 90 | 25 | – | 2.8 | 2.1 | 3 | 3.3 | A000400091A2AA0 | |||
| M 5 | 5 | 0.8 | 100 | 28 | – | 3.5 | 2.7 | 3 | 4.2 | A000500091A2AA0 | |||
| M 6 | 6 | 1 | 110 | 32 | – | 4.5 | 3.4 | 3 | 5 | A000600091A2AA0 | |||
| M 8 | 8 | 1.25 | 125 | 40 | – | 6 | 4.9 | 3 | 6.8 | A000800091A2AA0 | |||
| M 10 | 10 | 1.5 | 140 | 45 | – | 7 | 5.5 | 3 | 8.5 | A001000091A2AA0 | |||
| M 12 | 12 | 1.75 | 180 | 50 | – | 9 | 7 | 3 | 10.2 | A001200091A2AA0 | |||
| M 14 | 14 | 2 | 200 | 56 | – | 11 | 9 | 3 | 12 | A001400091A2AA0 | |||
| M 16 | 16 | 2 | 200 | 63 | – | 12 | 9 | 3 | 14 | A001600091A2AA0 | |||
| M 18 | 18 | 2.5 | 220 | 63 | – | 14 | 11 | 3 | 15.5 | A001800091A2AA0 | |||
| M 20 | 20 | 2.5 | 250 | 70 | – | 16 | 12 | 3 | 17.5 | A002000091A2AA0 | |||
| M 22 | 22 | 2.5 | 280 | 80 | – | 18 | 14.5 | 3 | 19.5 | A002200091A2AA0 | |||
| M 24 | 24 | 3 | 280 | 80 | – | 18 | 14.5 | 3 | 21 | A002400091A2AA0 | |||
| M 27 | 27 | 3 | 315 | 90 | – | 20 | 16 | 3 | 24 | A002700091A2AA0 | |||
| M 30 | 30 | 3.5 | 315 | 100 | – | 22 | 18 | 3 | 26.5 | A003000091A2AA0 | |||
Features
Thread type
ISO Metric corse thread
Geometry
Tap with straight flutes
Type of chips
Medium to long chipping
Material
Conventional high speed steel

Through Coolant
Machine nut taps
Direction of cut
Right
Application Range
P
Steel
| MG | Use | Speed [m/min] | Material examples |
|---|---|---|---|
| P.1 | 18-20 | + Show examples | |
| P.2 | 15-18 | + Show examples | |
| P.3 | 12-15 | + Show examples | |
| P.4 | 10-12 | + Show examples |
Legend
- Recommended
- Suitable
Cutting parameter calculation
Cutting speed m/min
Rotational speed
0 Rpm
Torque
0 Nm
Spindle power
0 W